Skip to content Skip to content

Slitting Production Scenarios for Machine Selection
Compare the production scenarios below with your own slit width mix, roll diameters, material sensitivity, and quality requirements. They help plant owners, purchasing teams, and technical managers prepare the information needed for a machine review.
These illustrative production scenarios outline common purchasing goals, process risks, machine review points, and RFQ inputs. Use them to describe your requirements; they do not report measured results from individual customer installations.

Scenario 1: PVC Edge Banding Converter Expanding SKU Count
When a PVC edge banding converter adds more widths and decorative finishes, slit edge quality, rewind hardness, and width changeover become central to the machine review. The configuration should be assessed against the usual order mix.
- Buyer target: increase finished width variety without losing consistent slit appearance or efficient changeover on narrow programs.
- Process risk: the old line runs one standard width well enough, then becomes unstable when mixed orders, decorative finishes, or frequent knife changes enter the schedule.
- Machine review: review knife repeatability, web path stability, and rewind control against the real width list rather than against one easy sample roll.
- RFQ inputs: send master width, thickness range, finished slit program, rewind diameter target, finish type, and the current defect that is forcing the project forward.

Scenario 2: Film Converter Running Mixed Orders On One Line
Mixed film orders require a review of the complete material range, tension requirements, finished roll quality, and changeover frequency. Identify the most sensitive film and the production condition that currently limits output.
- Buyer target: handle more than one film structure and more than one roll program on the same slitter rewinder without creating wrinkles, telescoping, or unstable rewind build.
- Process risk: the operating window is wider than the original line configuration, so instability shows up when the order changes rather than during a single sample run.
- Machine review: judge the proposal around the most sensitive material, largest unwind diameter, and highest finished roll demand in the real order mix.
- RFQ inputs: separate film families by difficulty, then send thickness range, roll sizes, slit widths, target speed, and the defect currently limiting output.
Do not compare machine names before you compare your real roll data
The faster route to a serious quotation is to send width mix, thickness range, unwind and rewind diameters, finish sensitivity, and the defect you want to remove. That is more useful than asking whether a line is “high speed” or “automatic.”

Scenario 3: Foil Or Laminated Material With Tight Slit Tolerance
Higher-value foil and laminated structures punish vague specification. In this type of inquiry, the machine can technically run while the finished product still fails downstream quality standards.
- Buyer target: reduce burr, dust, stretch, or surface marking where quality complaints cost more than moderate speed loss.
- Process risk: knife suitability, alignment stability, and roll support are underspecified, so scrap appears later in printing, lamination, or converting.
- Machine review: the quotation should focus on quality control points, not only on nominal width and speed claims.
- RFQ inputs: include tolerance expectation, acceptable defect level, surface sensitivity, roll sizes, and when the current defect becomes visible in production.
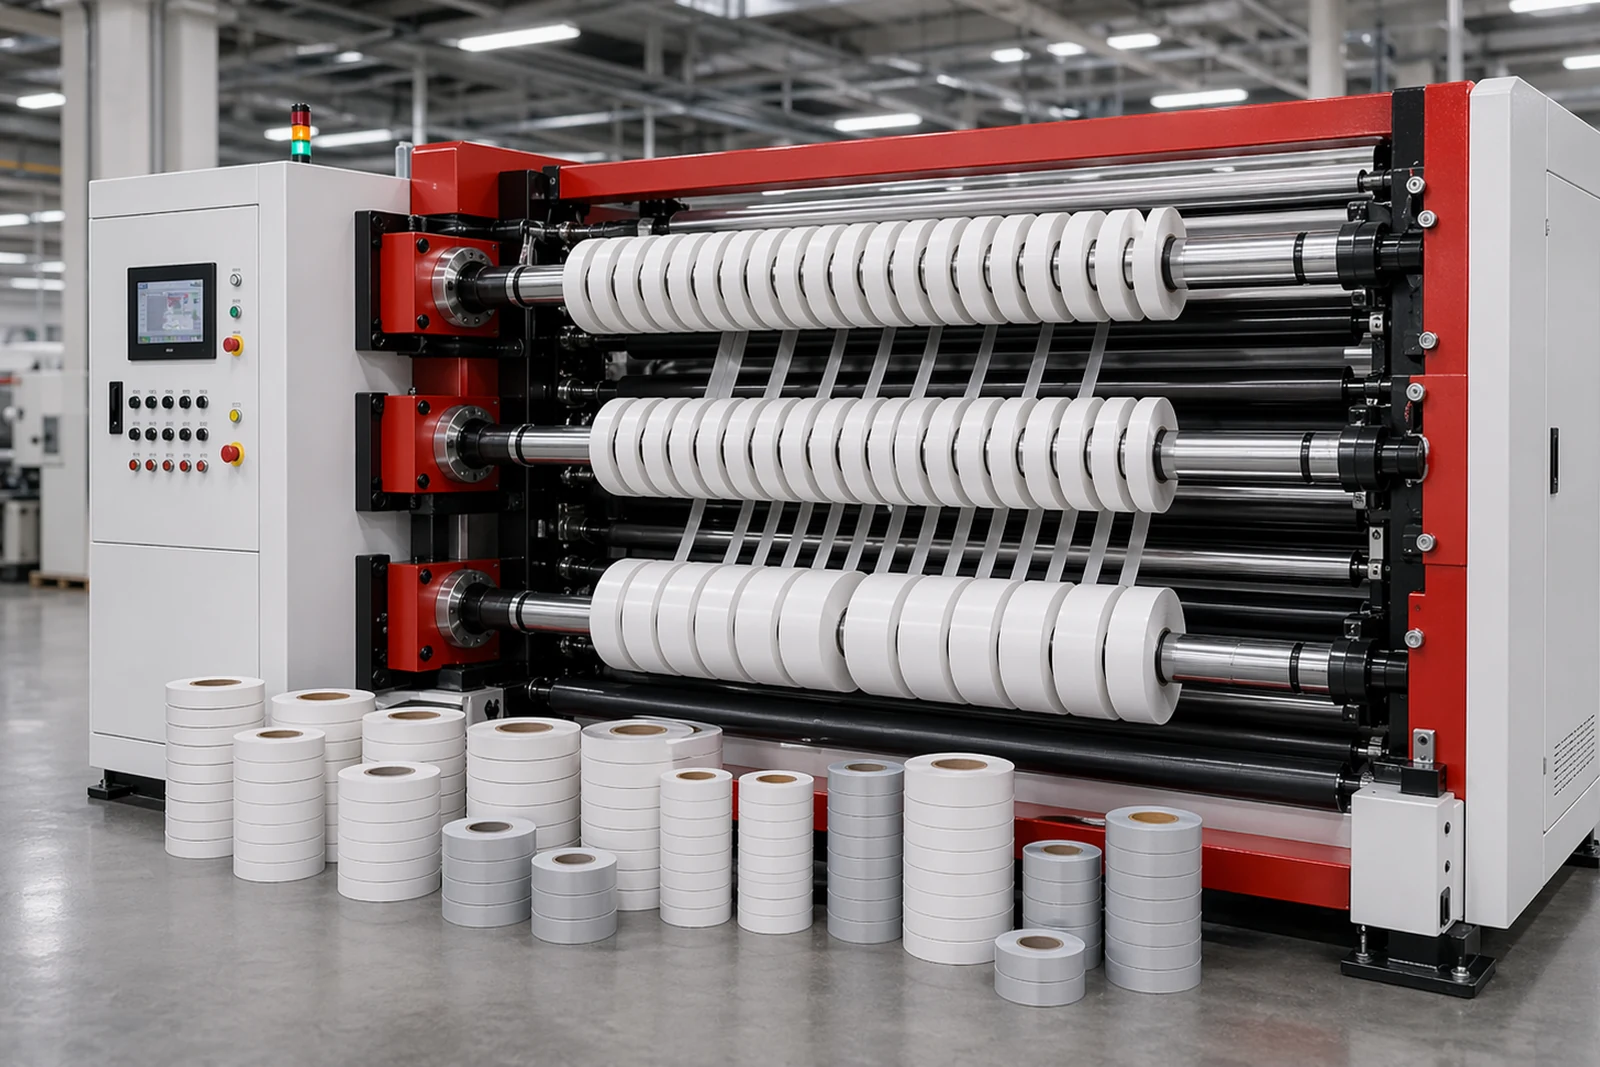
Scenario 4: Paper Or Labelstock Converter Balancing Throughput And Roll Quality
Paper and labelstock buyers often ask for more throughput, but the real commercial question is stable weekly output across repeat jobs, not brochure speed on one ideal specification sheet.
- Buyer target: improve usable plant output without sacrificing slit cleanliness, roll build quality, or operator efficiency across recurring jobs.
- Process risk: dust, uneven rewind build, and setup loss are treated as operating issues even though they are frequently tied to how the machine is specified.
- Machine review: review shaft arrangement, knife setup rhythm, daily order pattern, and target diameters against the actual production schedule.
- RFQ inputs: send basis weight or thickness range, master width, finished width mix, average order size, and the bottleneck you want the new line to remove first.
Need a capability review before you ask for price?
If procurement and engineering are not aligned yet, compare materials and applications first, then check capabilities, then send the RFQ. That sequence usually removes the low-quality back-and-forth that slows industrial machine buying.
Questions Procurement And Engineering Should Align On
- Which material and job mix defines the hardest production condition?
- Which defect or performance limit is the plant trying to eliminate first?
- Which widths, diameters, and thicknesses represent normal production instead of a single sample order?
- Is the new line for replacement, capacity expansion, or a new application?
- Does the buyer need a standard layout or a more specific machine scope?
What To Include In A Serious Slitter Rewinder Inquiry
- Material family and thickness range
- Master roll width and maximum unwind diameter
- Finished slit width list and target rewind diameter
- Expected speed or daily output goal
- Current defect or operating problem to solve
- Whether the machine is for replacement, expansion, or a new converting line
Next Step
Use the closest scenario above as a starting point, then compare it against your own order mix and plant constraints. If you send material family, width range, roll diameter requirement, and the problem you want to solve, GX Slitting can respond with a more realistic machine direction instead of a generic catalog answer.